
Know the next eight hours. Own every action in them.

Plant Toolbox lays out each shift's work before it starts, helps your team turn every miss into an owned action on a tiered action plan, and judges that plan with decision models you can read and test. Operators, maintenance, quality, safety and planning start the shift knowing what's coming and who owns it.

  • Operators
  • Maintenance
  • Quality
  • Safety
  • Planning

Production line. Illustrative concept drawing of a bottling line: Line 4's filler, labeler and case packer, with an operator at the filler and maintenance at the labeler. Plant Toolbox at work here: Line 4 filler (Running): Rate 182 /min; Good count 35,140; OEE 71.4%, goal 78.0; Next C/O 11:16, in 96 min. CIL, conveyor: Chain lube, due 10:30; Time left 50:00.

Machine shop. Illustrative concept drawing of shop-based manufacturing: unlike machines with one operator each, a job routed from Saw 1 to Mill 3, and the shift's huddle at the plant board. Plant Toolbox at work here: Plant Downtime: OEE, stops, minors by machine. 09:30 huddle raised #4180. Saw 1 (Stopped): Since 09:31 9:00; Reason blade, worn; Action #4180, Marcus Lee; Due Thu. Lathe 2 status: Changeover 14:00 of 35 min.

Processing. Illustrative concept drawing of batch manufacturing: an operator adding citric acid at the manway of a 30,000 kg mix tank on a steel deck, and a hold tank that your CIP controls are cleaning. Plant Toolbox at work here: Mix Tank 1, S26-0412: Order 40% complete; OPR03, citric acid 180 kg; Limits LL 178.2, UL 181.8; Step time 4:10. Locked by Nikhil Rao. Cleaning Order: CL26284-9WRB, in progress.

Keyboard: use the arrow keys to step through.

Illustrative · conceptProduction line · Harbor Point Plant, 09:40Machine shop · Fairport Plant, 09:40Processing · Harbor Point Plant, 09:40
How a miss becomes an action

In use on the plant floor at

“The sky is the limit, and Plant Toolbox is going to help us get there.”

Luke D., Head of Operations, Opella
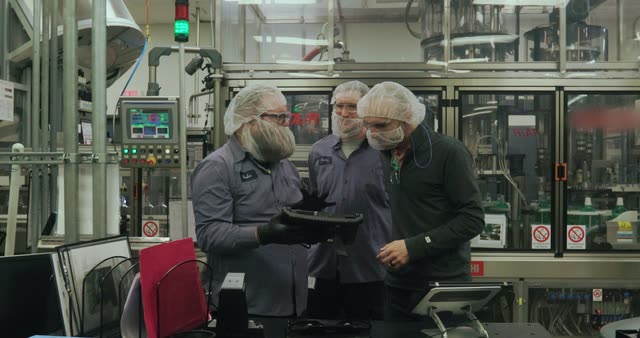
Three operators in hairnets around a tablet at a packaging line Watch the Opella story · 3:40

Opella · a Plant Toolbox customer story

One loop for the whole plant: Plan, Do, Check, Act.

Every area sets its goals. The crew works the inputs that move them, results are measured live and as KPIs, and decision models show where to adjust the plan before the loop runs again. Plant Toolbox also checks whether each action moved the number.

See every decision model
  1. 01

    Plan

    Set goals across the entire platform. Every area, from Operations, Quality and Safety to Maintenance and Inventory, can put a goal on any KPI, in any module.

    Line 4Week 41 plan

    • DOEE≥ 78.0%
    • QRight 1st Time≥ 98%
    • CCIL completed≥ 95%

    Goals Score Card Supply Stream Inventory

  2. 02

    Do

    The inputs a site controls: centerlines, CILs, the skill matrix, health checks and the owned actions on every board. This is the work that moves the goals.

    Line 4Shift A · 2 of 3 done

    Centerline Audit CIL Event Execution Skill Matrix Escalate

  3. 03

    Check

    Results are measured two ways: live, with counts about every 10 s and each stop traced to its machine, and as KPIs tracked across every module.

    Most monitoring tools stop here. They measure, and nothing else happens.

    Line 4Score Card · OEE

    71.4%Off target

    Score Card KPIs Related Downtime Events Did the actions work?

  4. 04

    Act

    Decision models judge each result against its goal and flag gaps no one owns. The team adjusts the plan, with Vera's briefing if the site uses it, and the loop starts again.

    Line 4KPI status · coverage

    Was: OEE · goal 78.0%, Off target · no action

    Now: Plan adjusted · #4182, OEE actions was none now 1

    KPI status coverage Decision Tree Vera briefing

Bring clarity to your operational teams before they leave the huddle.

Set at the 05:45 huddle: one schedule, every job on the line and who does it.

How the huddle sets the shift

Harbor Point Plant · Line 4 · Bottling

Mon Oct 12, 2026 · Shift A 06:00–14:00 · Now 09:40

Illustrative · concept

  1. 05:45 Pre-shift huddle · Green 85, on the Line Action Plan, before the shift Leader Done

    Maya Chen Line lead

  2. 06:00 Safety walk, planned for the start of the shift, 06:00 to 06:20 Safety Done

    Dana Ruiz EHS lead

  3. 06:00 Lemon Zest, then Sparkling Lime: B26-1186 Lemon Zest 12 oz × 24, 06:00 to 11:16, then B26-1187 Sparkling Lime 12 oz × 24, released, from 11:51 into Shift B Production Running

    Ana Souza Operator, with Marcus Bell and Tran Nguyen

  4. 06:15 3 CILs · 1 defect → WO-5527, 06:15 to 06:40: the filler infeed starwheel inspection found a defect; WO-5527 Filler infeed starwheel stays open for Shift B Maintenance Done

    Marcus Bell Operator

  5. 07:00 Cap torque and fill level: cap torque every hour, 07:00 to 13:00; fill level every 2 hours, 08:00 to 12:00; 07:00 to 09:00 done Quality Due 10:00

    Tran Nguyen Operator

  6. Now 09:40
  7. 11:16 Changeover to Sparkling Lime: from B26-1186 Lemon Zest, 11:16 to 11:51, target 35 min, three tasks Changeover 1 work order Planned

    • Changeover: Flavor change, Tran Nguyen, Operator
    • Maintenance: Labeler vacuum pump: WO-5521, inspection moved up from 13:00 into this stop, Luis Ortega, Maintenance tech
    • Maintenance: 2 CILs, during the changeover, Marcus Bell, Operator
  8. 11:51 First-off check, B26-1187, after the changeover, 11:51 to 12:06 Quality Planned

    Priya Nair Quality engineer

  9. 13:45 Handover to Shift B, 13:45 to 14:00 Leader Planned

    Maya Chen Line lead

Modules behind this view

  • Line Action Plan
  • Process Confirmation
  • Line Production Schedule
  • CIL Event Execution
  • Production Execution
  • Changeover Task List
  • Maintenance Work Orders
  • Shift Handover
A concept built from shipped modules. One work order per changeover is proposed, not shipped.

One plan, every tier.

Escalate for the decision. De-escalate to get it done.

A worn filler starwheel costs Line 4 about three hours a week, and a new one costs $18,400. Follow action #4207 up to the plant for the spend and back down to the line for the fix.

Harbor Point Plant · Line 4 · Bottling

Arrow keys: step through the moments.

Line 4 from the depalletizer to the case packer: at the filler, bottles jam at the infeed starwheel and the shift team logs the loss Maintenance shop with a drill press and a lathe: the lead tech points at the OEM quote on the bench monitor while two techs talk it over Plant board room: the plant team sits around the conference table while the plant manager approves the $18,400 spend on the wall screen Maintenance shop: the starwheel set is on order, PO 4500-2231, and the lead tech checks the delivery date Line 4 at the filler: a maintenance tech fits the new starwheel while the line lead watches, and the stack light is green

LineLine 4 finds the lossFiller infeed jams, nine weeks running. The crew logs the loss and the part, but a new starwheel is above line authority.

Department · MaintenanceMaintenance prices the partThe OEM quote is $18,400 with a 3-week lead, over the $5,000 department limit.

PlantThe plant approves the spendPayback is about 2.5 weeks of the loss. Approved, and sent back down to buy it.

Department · MaintenanceMaintenance buys the partPO 4500-2231 is raised; the set arrives Nov 11.

LineLine 4 installs itFitted on the Nov 18 changeover. The loss drops to 22 min a week, under the goal of 30.

#4207 created on the Line Action Plan · Line 4.

#4207 escalated to the Department Action Plan · Maintenance.

#4207 escalated to the Plant Action Plan · Harbor Point.

#4207 de-escalated to the Department Action Plan · Maintenance.

#4207 de-escalated to the Line Action Plan · Line 4.

Line Action Plan › Line 4Department Action Plan › MaintenancePlant Action Plan › Harbor Point

#4207

Replace the worn filler infeed starwheel

Line Action Plan · Line 4Department Action Plan · MaintenancePlant Action Plan · Harbor Point

Blocked · needs a quoteBlocked · over limitApprovedOn orderDone · goal met Unplanned DT · FillerDue Nov 18
  1. Maya Chen · Mon, Oct 12 · 6:40 amNew

    Filler infeed jams for nine weeks, about 186 min a week. Starwheel worn 2.4 mm.

  2. Maya Chen · 6:52 amNew

    A new starwheel set is above line authority. Escalating to Maintenance for a quote.

    Sub-action: Get a quote for the infeed starwheel and guide set

    Assigned to Luis OrtegaDue Oct 14OpenDone

  3. Luis Ortega · Wed, Oct 14 · 2:15 pmNew

    OEM quote Q‑55821: $18,400, 3‑week lead. Over our $5,000 limit, so it goes to the plant.

    Sub-action: Approve the $18,400 spend

    Assigned to Sam WhitfieldDue Oct 21OpenDone

  4. Sam Whitfield · Wed, Oct 21 · 9:30 amNew

    Payback is about 2.5 weeks of the loss. Approved. Back to Maintenance to order it.

    Sub-action: Raise the PO for the starwheel set

    Assigned to Luis OrtegaDue Oct 22OpenDone

  5. Luis Ortega · Thu, Oct 22 · 10:05 amNew

    PO 4500‑2231 raised. The set arrives Nov 11.

    Sub-action: Fit the new starwheel on the Nov 18 changeover

    Assigned to Maya ChenDue Nov 18OpenDone

  6. Maya Chen · Wed, Nov 18 · 3:20 pmNew

    Fitted on the changeover. Down to 22 min a week, under the goal of 30. Closing.

Open on Line AP
Open on Dept AP
Open on Plant AP
Open on Dept AP
Open on Line APEscalate

Line 4 filler · lost min a week

186 a week 186 a week · over goal 186 a week · approved 186 a week · on order 22 a week · under goal

Line chart of Line 4 filler lost minutes, a 7-day rolling total for each day of weeks 33 to 49. It runs between about 177 and 196 minutes a week, far above the goal of 30, until the new starwheel is fitted on Wednesday of week 47, then falls through the next week and settles between 20 and 26, under the goal. The line is red above the goal and green at or below it.

Start with one line and one shift.

Bring one line and one shift pattern. In a 60-minute demo we walk a shift in Plant Toolbox: the work due by role, the decision models that judge the plan, from the pre-shift Decision Tree to a KPI miss, and the actions with their owners.

Need IT on board first? Send them the trust page